Lamp fogging is influenced by assembly moisture, vapor transport, ventilation paths, temperature distribution and the inner surface of the lens.
Moisture enters through assembly and environment
Components and adhesives can introduce moisture during assembly, while ambient humidity enters through air exchange. Rapid lens cooling can then move the surface below the local dew point.
Ventilation controls whether moisture can leave
Breather location, airflow and seal condition affect drying after a temperature cycle. If liquid water enters continuously, the amount of condensation a surface coating can manage is necessarily limited.
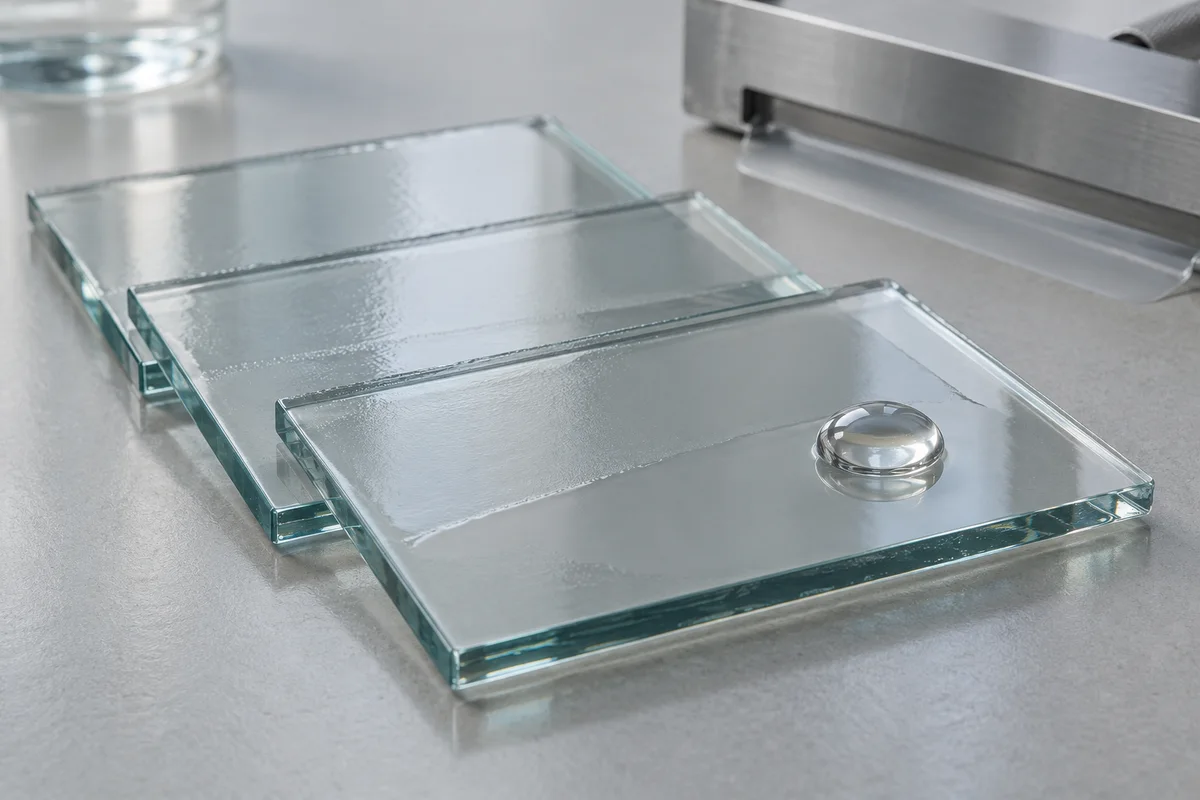
An anti-fog surface manages the lens interface
A hydrophilic coating changes condensate morphology and reduces scattering from fine droplets, but it must remain compatible with the clear substrate, pretreatment, application and cure.
Condensation location and moisture sources
Local lamp condensation needs to be mapped against operating conditions. Cold regions, vent-adjacent areas and assembly edges may experience different moisture behavior. Material comparisons should reflect product-level locations and temperature conditions rather than only an easily coated flat area. Persistent moisture accumulation may remain an issue even when surface wetting improves.
Contact with assembly materials
A coated transparent part may contact adhesives, seals or cleaning residues. These interactions belong in compatibility evaluation. Assembly can introduce local contamination, adhesion changes or optical marks not seen on isolated coupons. Matched images before and after assembly, with uncoated and existing-material controls, help distinguish coating, assembly and contact-media effects.
Validation at material, component and lamp levels
Material-level work addresses film formation, adhesion and condensation appearance. Component-level work addresses curved-surface coverage, edges and assembly compatibility. Lamp-level validation includes thermal, ventilation and optical systems. These records should connect but are not interchangeable. Functional-coating development supports the material stage; finished-lamp safety, performance and conformity remain product-validation responsibilities.
Our service connects the material with the application process
Organic Advanced Materials can support hydrophilic anti-fog materials and application conditions for transparent parts. Lamp sealing, ventilation and full-system reliability remain the shared responsibility of the relevant design and manufacturing teams, preventing a system problem from being misidentified as a coating-only issue.
Development and acceptance criteria
| Evaluation area | Evidence to retain |
|---|---|
| Exposure location | Cold regions, vent-adjacent areas and assembly edges. |
| Contact materials | Controls for adhesives, seals and cleaning residues. |
| Validation levels | Separate material, curved-component and complete-lamp conditions. |
For anti-fog materials for vehicle-lighting components, share the lighting substrate, assembly conditions and condensation cycles. Our team will confirm the material direction, sample conditions and applicable technical documents.
Technical enquiry →